Hey there, welcome back to the shop—today I’m breaking down something most folks don’t think about: what really goes on inside an automatic paint line, especially when you’re working with a supplier that’s got your back (that’s us, by the way). A lot of people just see a conveyor belt with parts zipping by and paint coming out, but it’s way more than that—those techniques aren’t just fancy tricks, they’re science wrapped in practical stuff that saves you time, money, and headaches. Let’s dive in, keep it real, no boring jargon here. Automatic Paint Line

First off, let’s get one thing straight: automatic paint lines aren’t one-size-fits-all. The techniques we use depend on what you’re painting—auto parts, appliances, metal cabinets, even plastic consumer goods. But the core methods are pretty consistent, and each has a reason it’s the go-to. Let’s start with the big one: electrostatic spray painting. This is the backbone of most automatic lines, right? Here’s how it works, dumbed down. The paint nozzle’s charged with a negative voltage, and the part on the conveyor’s grounded (positive). Opposites attract, so every paint droplet flies straight to the part instead of drifting all over the place. I’ve seen this cut paint waste by up to 30% compared to manual spraying—game changer for shops that don’t want to toss half their paint can. But wait, there’s a trick here: we don’t just crank the voltage to max. Too high, and you get “electrostatic overspray” where paint clumps up in weird spots, or even arcing (that’s like a tiny spark, not good for flammable paint). Our techs calibrate the voltage based on the part’s size—small plastic knobs get less, big metal truck frames get more. That’s the stuff a lot of new suppliers miss, but we’ve been refining this for years.
Next up: airless spray painting. Yeah, it sounds counterintuitive—airless, no air? Basically, we push paint through a tiny nozzle at super high pressure (like 1,000 to 3,000 PSI) to atomize it into fine droplets, no compressed air needed. This is perfect for thick paints, like primers or textured finishes (think a rugged fridge exterior). Why use this over regular spray? It’s faster, covers more surface area in one pass, and doesn’t mess up thin parts—no air blowing delicate plastic out of alignment mid-paint. But here’s the catch: if the pressure’s off, you get a lumpy finish. Our automatic systems have pressure regulators that adjust in real time, so even if the part moves slightly on the conveyor, the paint flow stays consistent. We also use heated lines for some airless setups—thick paint gets sticky when it’s cold, so heating it keeps it flowing smoothly without clogging nozzles. Clogged nozzles = downtime, and we hate downtime more than you do.
Wait, let’s not sleep on powder coating. A lot of people mix powder coating with paint, but it’s a different technique, and we integrate it into a bunch of our automatic lines. Instead of liquid paint, we use dry powder particles (usually polyester or epoxy) that get charged electrostatically, same as spray. The part goes into an oven, and the powder melts, flows out, and cures into a hard, durable finish. This is huge for metal parts that take a beating—auto wheels, exercise equipment, outdoor furniture. Why is powder coating better than liquid here? No solvents, so it’s way more eco-friendly (no toxic fumes to vent out), and the finish is tougher, resists scratches and chipping way better. Our automatic powder coating lines have built-in reclaim systems, too—any powder that doesn’t stick to the part gets sucked up, filtered, and reused. That cuts waste to almost zero, which saves customers thousands a year in material costs. I’ll be honest, we pushed for that reclaim tech a few years back because so many clients were complaining about powder waste, and now it’s standard on all our lines.
Now, pre-treatment—this is a step most suppliers skip talking about, but it’s make-or-break for paint adhesion. If you don’t clean the part right, the paint’ll peel off in a month, no matter what technique you use. Our lines have a 3-step pre-treatment process: first, a degreaser wash to get rid of oil, dirt, or machining residue, then a rinse with clean water, then a conversion coating (like zinc phosphate) that bonds to the metal (or a plasma treatment for plastics) so the paint sticks. A lot of cheap lines cut corners here—just a quick spray and call it a day—but we do the full thing because we’ve seen what happens when they don’t: callbacks, rework, lost business. That’s why our clients stick around; we don’t just sell equipment, we make sure their paint jobs last.
Then there’s automated brush or roll coating—wait, who uses that? Mostly for flat, thin parts, like metal sheets for cabinets or signs. Instead of spray, we have rotating brushes or rollers that apply an even coat of paint as the part moves along the conveyor. This is super consistent, no drips or runs, which is perfect for large, flat surfaces where spray might leave overlapping marks. The trick here is matching the brush material to the paint—if you use a hard brush with a latex paint, it’ll leave streaks. We test each setup with the client’s specific paint before installing, so they don’t have to figure that out on their own. It’s not as flashy as spray, but for certain jobs, it’s way better.
Now, let’s talk about how these techniques work together in a full line. A typical auto line we install goes like this: unload parts → pre-treatment wash → dry → maybe a primer coat (usually electrostatic spray) → cure the primer → top coat (either airless, electrostatic spray, or powder coating) → cure the top coat → cool down → unload. Each step is timed to the conveyor speed, so parts don’t sit around too long or rush through a step. We use PLC (programmable logic controller) systems to run all this—you can set it up on a touchscreen, adjust voltage, pressure, cure times, all from one place. No more tweaking knobs manually for every part; the system remembers the settings for each part type. That’s a huge efficiency gain—manual lines need an operator to adjust stuff, but our lines run with minimal oversight. We even add sensors that catch if a nozzle’s clogged or paint level’s low, so the line can pause before messing up a batch of parts.
Wait, common myths here: some people think automatic paint lines only do one color, but nope. We have color change systems that flush the paint lines with a cleaning solvent (or just water for water-based paints) in seconds, so you can switch from red to blue without wasting a bunch of paint. A lot of suppliers use old systems that take 10 minutes to change colors, but our tech cuts that to 2 minutes. That’s perfect for clients that do small runs of multiple colors—no need to wait around, no wasted paint. Also, water-based vs. solvent-based paints: our lines handle both. We have separate exhaust systems for solvent-based because they’re flammable, and better filtration for water-based to cut down on waste. We don’t force clients to use a certain paint; we adjust the line to work with whatever they’re already using, because we know switching paint types is a hassle.
Now, why does this matter to you? If you’re running a small shop and thinking about upgrading from manual paint, or a big manufacturer looking to scale, the techniques we use aren’t just about getting a pretty finish—they’re about reducing labor, cutting waste, and increasing quality. I once had a client who was spending $12k a month on paint waste with their manual line; we installed an automatic electrostatic line with reclaim, and their paint cost dropped to $4k a month. That’s real numbers, real savings. Another client had issues with paint peeling on metal bike frames; we fixed their pre-treatment step and switched to powder coating, and their return rate went from 8% to 0. That’s the stuff that makes our job worth it.
But here’s the thing: every client’s needs are different. A line that works for auto parts won’t work for plastic toys, and vice versa. That’s why we don’t just show up with a pre-built line and say “good luck.” We walk through your facility, talk about what parts you paint, what volume you need, your budget, even your long-term goals—like if you’re planning to expand next year. Then we build a custom line with the right techniques, not a one-size-fits-all junk setup. We also offer training for your team, so they know how to adjust settings, fix small issues, and keep the line running smooth. No one wants to hire a fancy technician just to keep the line going.
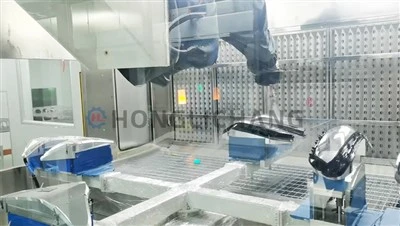
So, if you’re tired of manual paint lines that have inconsistent finishes, waste tons of paint, and eat up your labor hours, we’ve got you. Our automatic paint lines use the best techniques tailored to your needs, no fluff, no overpromising. Want to chat through what would work for your shop? Just reach out—we’ll break down the costs, the savings, and answer any questions you have, no sales pitch nonsense.
UV Coating Line References
- Robbins, A. (2021). Industrial Coating Technology: Fundamentals of Automatic Paint Systems. Manufacturing Press.
- Chen, L. (2019). Electrostatic Spraying for Industrial Applications. Journal of Coatings Technology and Research.
- Smith, K. (2020). Powder Coating Processes and Efficiency in Automated Lines. Surface Finishing Magazine.
- Industrial Automation Association. (2022). Best Practices for Pre-Treatment in Paint Lines.
Shenzhen Honglichang Machinery Manufacturing Co., Ltd.
We are one of the most professional automatic paint line manufacturers and suppliers in China, also support customized service. Please feel free to buy advanced automatic paint line for sale here from our factory. Welcome to contact us for quotation.
Address: No. A802, Building 2, Tianan Digital Plaza, Longgang, Shenzhen, China
E-mail: victor@honglichang.com
WebSite: https://www.honglichang-paint.com/
